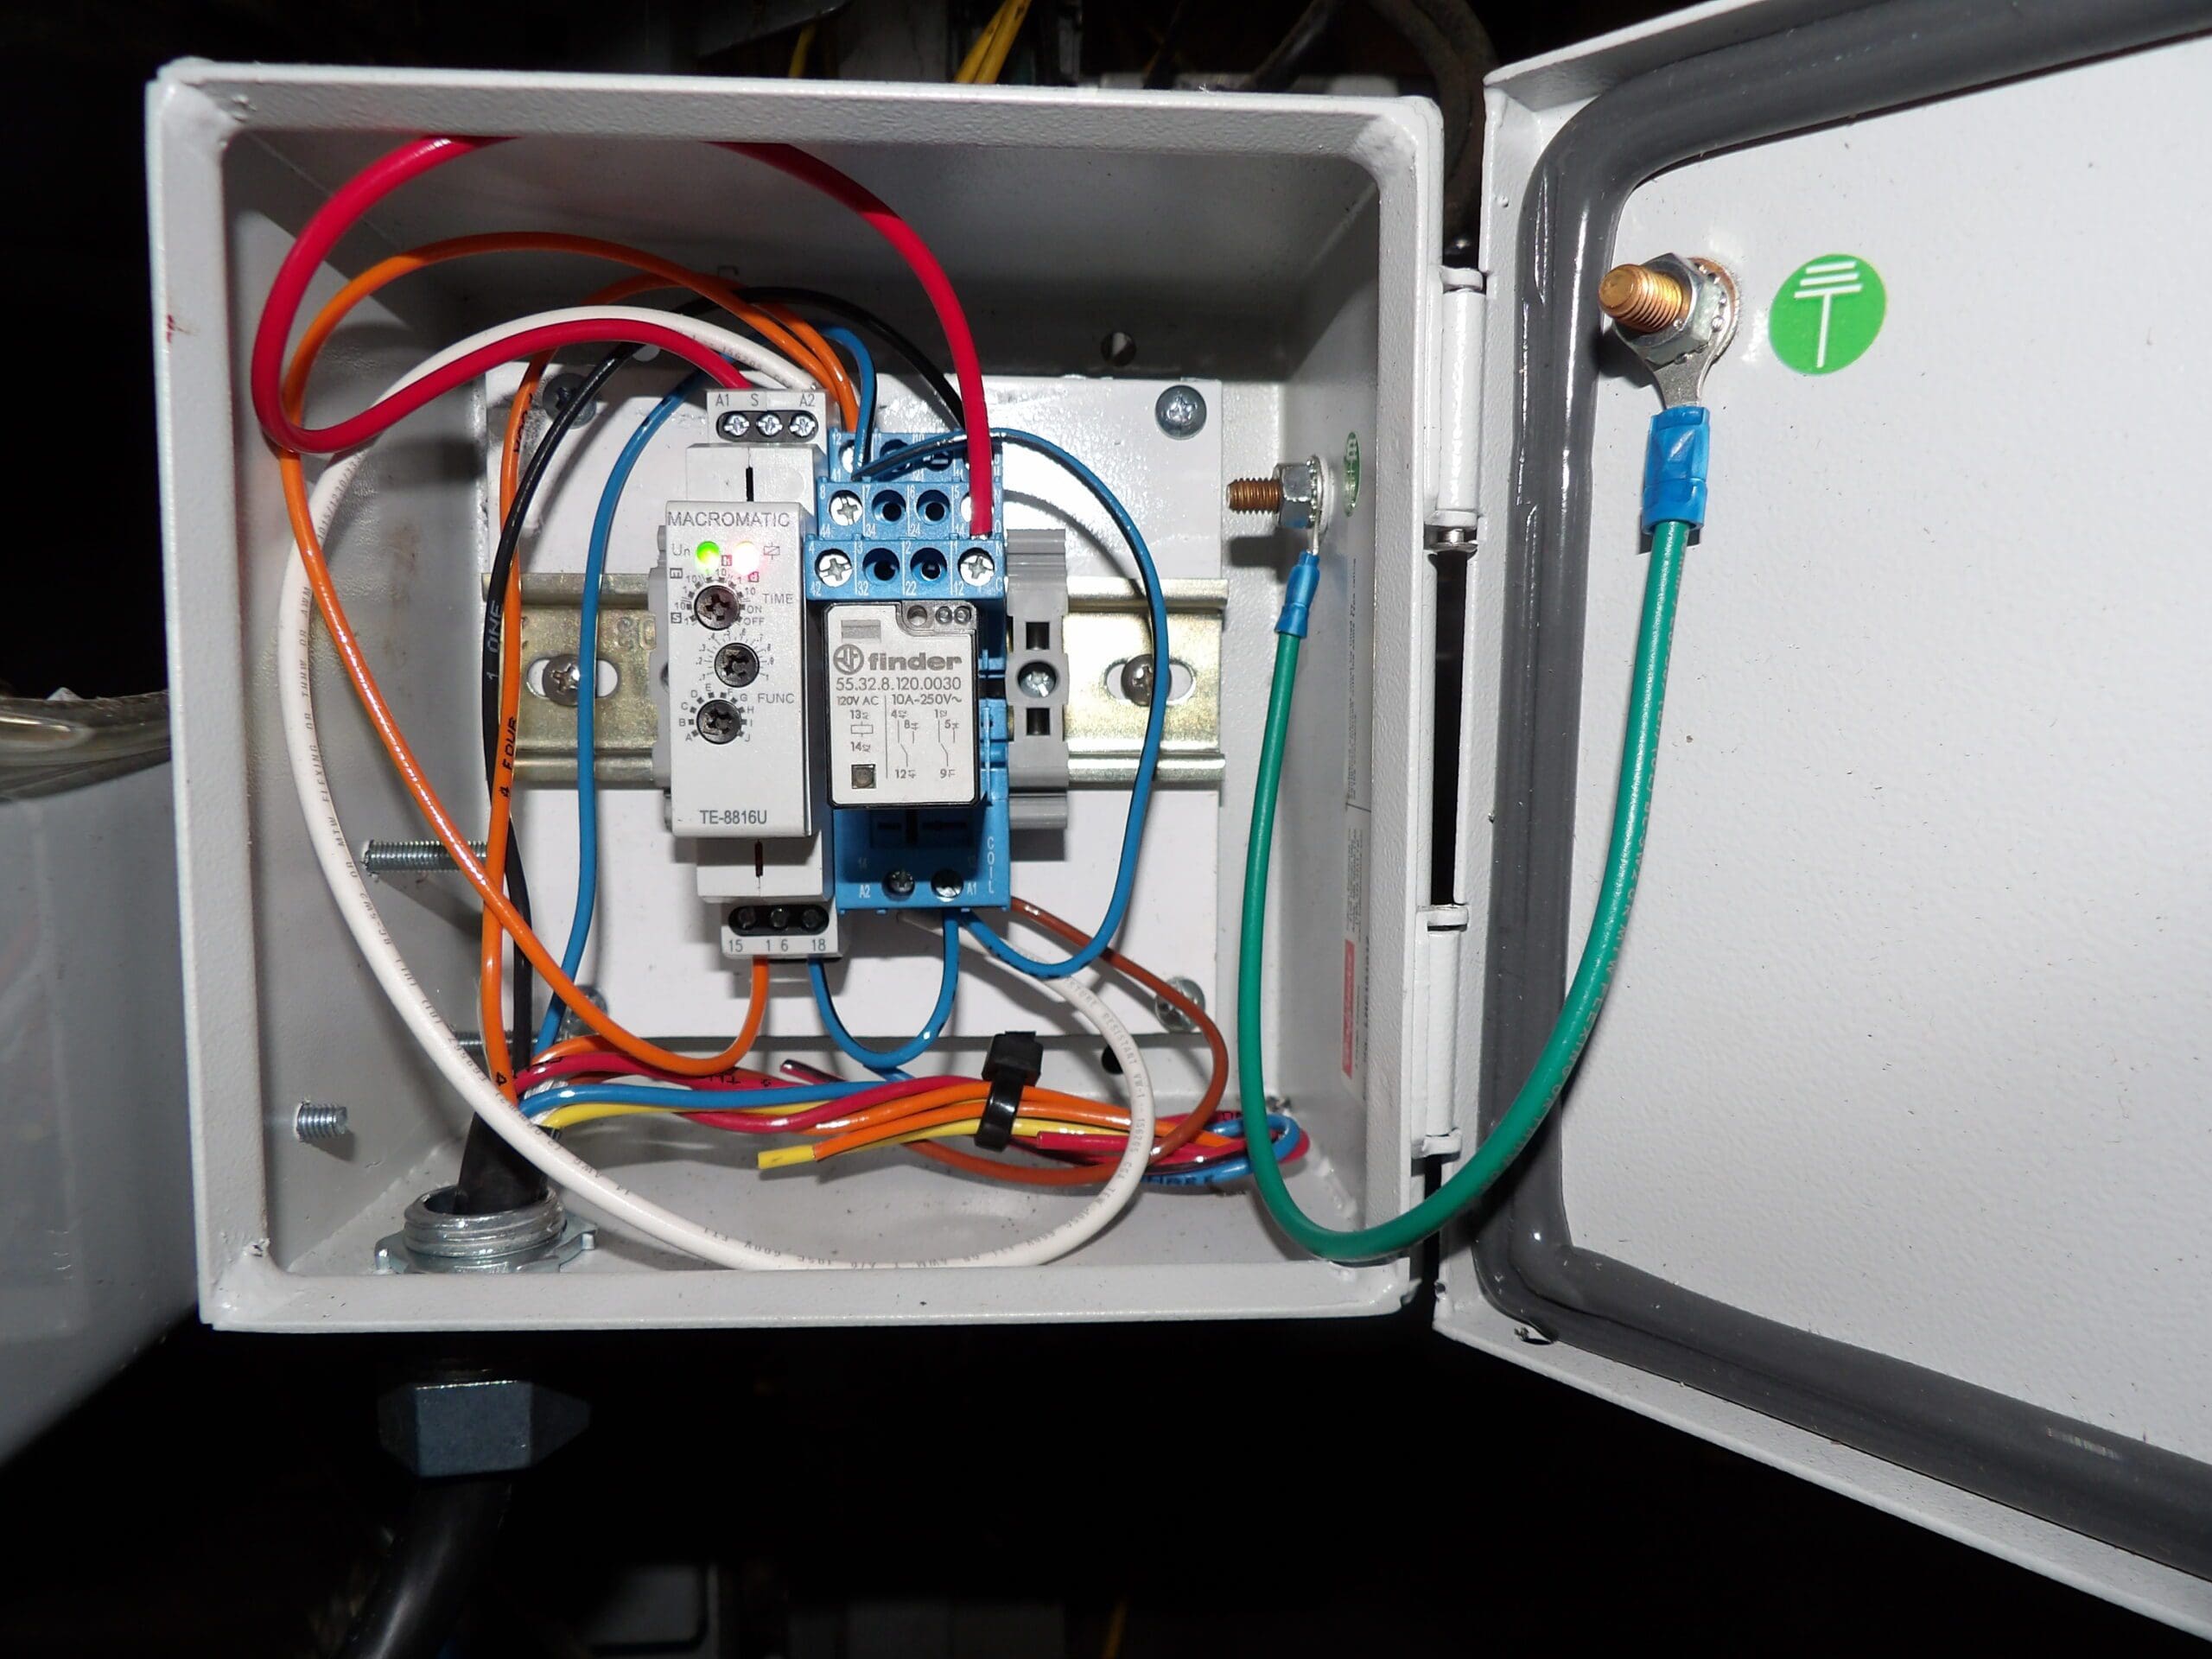
Our partner, Wynright, kept experiencing motor failures on hydraulic lift tables in their distribution centers. They asked that we get involved to help pinpoint the exact issue causing $160K a month in failed motors and hours of downtime. E Tech Group harness our expertise in material handling automation to diagnose and remedy this expensive issue.
Industry Challenge: High-Speed, High-Volume Logistics
In the parcel industry, throughput is everything — especially during peak seasons when daily package volume can double or triple. The client’s existing system faced mounting challenges, including:
- Aging PLC hardware prone to failure during high-demand periods
- Limited system visibility, slowing diagnostics and recovery
- Difficulty scaling to meet growing throughput demands
Any unplanned downtime during a peak shipping window could lead to major customer service disruptions and financial penalties.
Dysfunction: Overloaded Lift Table Motors
During the process review with the customer and distribution center associates, it was determined that the failures were likely due to excessive cycling of the on/off state of the motor. The cycling was a direct result of the hard contact of a foot switch provided to the line associates to raise the lift table.
Diagnosis: A Miscommunication Between Human & Machine
In a normal working position, the associate would stand with one foot on the switch and the normal shift of weight as packages are moved across the worker’s position would cause incidental switching of the motor. Some instances indicated that in an effort to perfectly position the lift table, the worker would feather start/stop operation, exacerbating the situation.
Treatment: Implement a Better Translational Tool
To remedy this initially, a VFD-based solution was recommended. But we felt a solution with a delay timer that negates the signal from the foot pedal for a short time, stopping the on/off signals would provide a better, more long-term resolution to their issue. Stewart Brinkoeter, our fabrication manager, partnered with our Ohio team to finalize and implement this solution in one facility for a test run.
A Tailored Control System Upgrade for Parcel Operations
E Tech Group designed and implemented a custom controls upgrade to meet the speed and reliability demands of parcel distribution. Key elements of the solution included:
- Migration to a modern control platform with increased processing power and diagnostic capability
- Integration with existing sorter and conveyor systems, maintaining compatibility while improving performance
- Updated HMI interfaces for intuitive operator control and real-time system feedback
- Redundant communication architecture to ensure continuous operation during hardware failures
The upgrade also included pre-deployment simulation to validate system behavior before going live.
Prognosis: An Elegant Solution to a Widespread Problem
Just an hour and a half of downtime and less than a third the cost of a new motor, the table was functioning flawlessly and the associate working with the test unit did not discern any loss of functionality. Because of its success, this solution will now be implemented across multiple distribution centers, offering Wynright a swift solution to what was a widespread, very expensive problem.